Solid carbide
5-flute end mills
One geometry, published across 5 diameters and two overall lengths. Dimensional data, part numbers, the AlTiN coating and the manufacturer’s cutting data are published for all 10 variants; substrate and carbide grade are pending final manufacturer confirmation.
- Diameters
- 6 · 8 · 10 · 12 · 16 mm
- Published variants
- 10
- Flutes
- 5
- Coating
- AlTiN
- ISO groups
- P · M · K · S
- Overall length
- 63 – 150 mm
Representative Z5 Series product photography. Dimensions vary by variant; refer to Specifications.

Family overview
One flute count across the range
Every published Z5 variant is 5-flute. Flute count is constant from ⌀6.0mm to ⌀16.0mm, so the choice within the series is diameter, reach and corner radius — not geometry.
Two overall lengths at every diameter
5 standard-length variants from 63 – 92 mm, and 5 extended-length (L) variants from 100 – 150 mm. Reach is selected without changing diameter or flute count.
Corner radius published per size
Corner radius is stated on every variant rather than quoted as a series figure, because it is not constant across the range. It appears in the table below and on each specification.
Cutting data, per diameter and per material
The manufacturer publishes slot and side milling parameters across ISO P · M · K · S — 9 workpiece material rows, each with its own speed, feed and engagement. They differ by diameter, so they are published on each variant’s own page rather than as a series figure.
What is not published yet
Substrate, carbide grade, helix angle and coolant recommendation are pending manufacturer confirmation — the data sheet names the coating and says nothing about what is under it. None is estimated here or anywhere else on this site.
Model shown: Z5 ⌀10.0mm
Inspect the released Z5 model directly in your browser. Published dimensions vary by variant.
Published specification for Z5 ⌀10.0mm →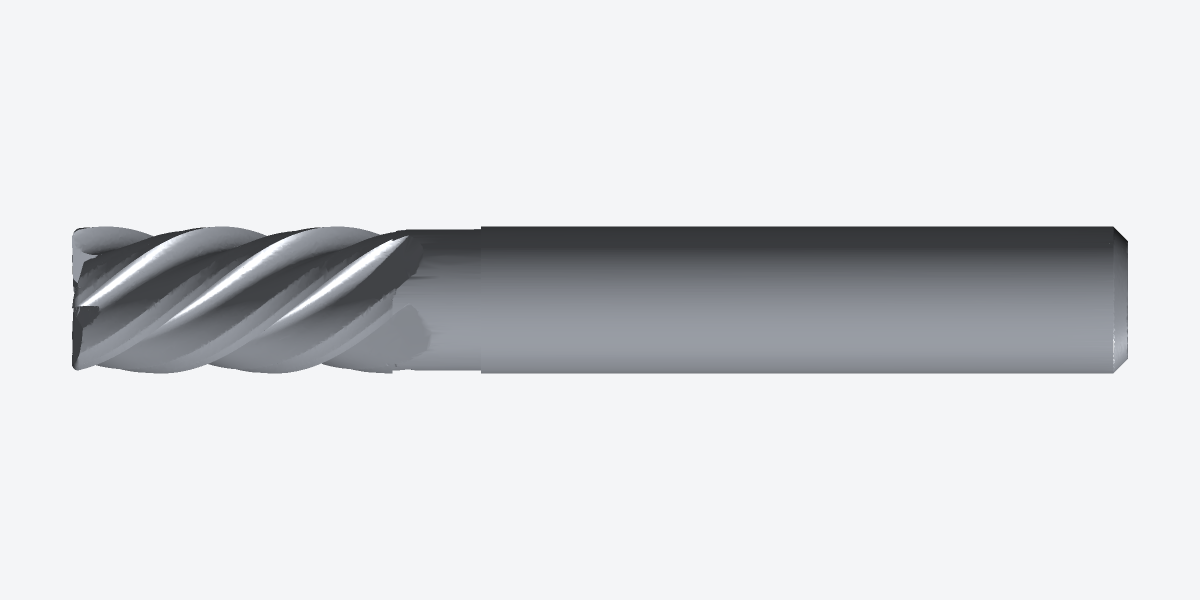
2.1 MB, loaded on request.
10 variants, two length classes
Standard length covers general milling reach. Extended (L) keeps the same diameter and flute count at a longer overall length, for depth the standard tool cannot reach.
Standard length
5 variants · 63 – 92 mm overall
Extended length — L
5 variants · 100 – 150 mm overall
Full published specification
| Variant | Shank | LOC | OAL | Corner Radius | Flutes | Action |
|---|---|---|---|---|---|---|
| ⌀6.0mm | 6mm | 12mm | 63mm | 0.3mm | 5 | |
| ⌀8.0mm | 8mm | 16mm | 63mm | 0.5mm | 5 | |
| ⌀10.0mm | 10mm | 22mm | 72mm | 0.5mm | 5 | |
| ⌀12.0mm | 12mm | 27mm | 83mm | 0.5mm | 5 | |
| ⌀16.0mm | 16mm | 32mm | 92mm | 0.5mm | 5 | |
| ⌀6.0mm L | 6mm | 15mm | 100mm | 0.3mm | 5 | |
| ⌀8.0mm L | 8mm | 18mm | 100mm | 0.5mm | 5 | |
| ⌀10.0mm L | 10mm | 22mm | 125mm | 0.5mm | 5 | |
| ⌀12.0mm L | 12mm | 22mm | 125mm | 0.75mm | 5 | |
| ⌀16.0mm L | 16mm | 30mm | 150mm | 0.6mm | 5 |
Every figure is read from the approved Z5 dataset. The AlTiN coating and the ISO P · M · K · S application range apply to the whole series and are not repeated per row; speeds and feeds differ by diameter and are published on each variant’s page. Substrate and carbide grade are pending final manufacturer confirmation. The identifier above is a part number — engraved on the tool and printed on the packaging as P/N. No SKU has been assigned and no barcode has been supplied.
What is published, and what is not
A specification a buyer can act on states its own gaps. These are the Z5 fields as they stand today.
Published for every variant
- Cutting diameter
- Shank diameter
- Length of cut (LOC)
- Overall length (OAL)
- Corner radius
- Flute count
- Part number (P/N)
- Coating — AlTiN
- ISO application group — P · M · K · S
- Workpiece materials and hardness bands
- Slot and side milling parameters, per diameter
Pending manufacturer confirmation
- Substrate · carbide grade
- Helix, rake and relief angles
- Coating thickness and hardness
- Coolant or dry recommendation
- ISO N and H suitability
- SKU · barcode
- Dimensioned technical drawing
Why they are empty
Each of these is a manufacturer statement, not an inference. A substrate grade can be guessed from a coating and a coolant strategy can be guessed from a material; both would be a specification claim this business has not made.
ISO N and H carry no row in the manufacturer’s data. That is an absence of guidance, and it is not published as unsuitability.
They appear on this site on the day the manufacturer supplies them, and not before. Document availability →
Reference material
General engineering reference — standard, publicly known machining formulas and classifications. These guides are not EUROCUTPRECISION cutting data: the manufacturer’s recommended parameters for Z5 tools are published on each variant’s own page, under Cutting data.
Tool Selection Guide
Flute count, corner radius, reach and rigidity — the decisions taken before a parameter is calculated.
Step-Over Guide
Radial engagement and the scallop-height calculation for finishing.
Hardness Guide (HRC)
The Rockwell C scale, typical bands and what hardness changes.
Cutting Speed Guide
Cutting speed (Vc) and spindle speed (RPM) formulas, and what decides the correct speed.
Request a quotation.
Specifications, quantity tiers and lead times are confirmed in writing against your enquiry.